
Dry food is highly sensitive to ambient moisture; poor sealing can lead to clumping, mold, and spoilage. Reliable dried food packaging helps protect products during storage and transit.

Packaging must use food-contact-safe materials and coatings, free from contamination risks and compliant with food safety regulations. Choosing an experienced food packaging manufacturer is essential.

Hermetic seals and container integrity help keep out insects, dust, and cross-contamination during storage and transit, supporting effective food packaging solutions.

Barrier properties against oxygen, light, and moisture help protect flavour, aroma, and nutritional quality over time, making industrial food packaging essential for dry food products.

Especially important for export and bulk B2B shipments where product trust needs to be verifiable on arrival.

Packaging should withstand handling, stacking, and long-haul logistics without deformation or breach.

The right container type for powders, granules, or whole grains supports efficient filling, settling, sealing, and custom food packaging requirements.
We bring global expertise, local understanding, and engineering precision together to deliver packaging solutions that keep dry food products fresh, pure, and shelf-stable.

Our packaging solutions are engineered with moisture-resistant seals and food-safe linings, purpose-built to keep grains, powders, and dry ingredients contamination-free across storage and transit.

Our food packaging solutions are manufactured under FSSC 22000 certification, ensuring globally recognised food safety management standards are met at every stage — giving dry food brands confidence in hygienic handling and regulatory compliance.

State-of-the-art production facilities with automated lines and precision processes, delivering consistent quality, accurate dimensions, and dependable sealing performance across batches of industrial food packaging.

Lacquer-lined and moisture-barrier coated packaging engineered to lock out humidity and contaminants, preserving freshness, flavor, and shelf life throughout the product's lifecycle.

From container sizing and closures to liner types suited to powders, granules, or whole-grain formats, Balmer Lawrie tailors custom food packaging solutions to each customer's product and export requirements.
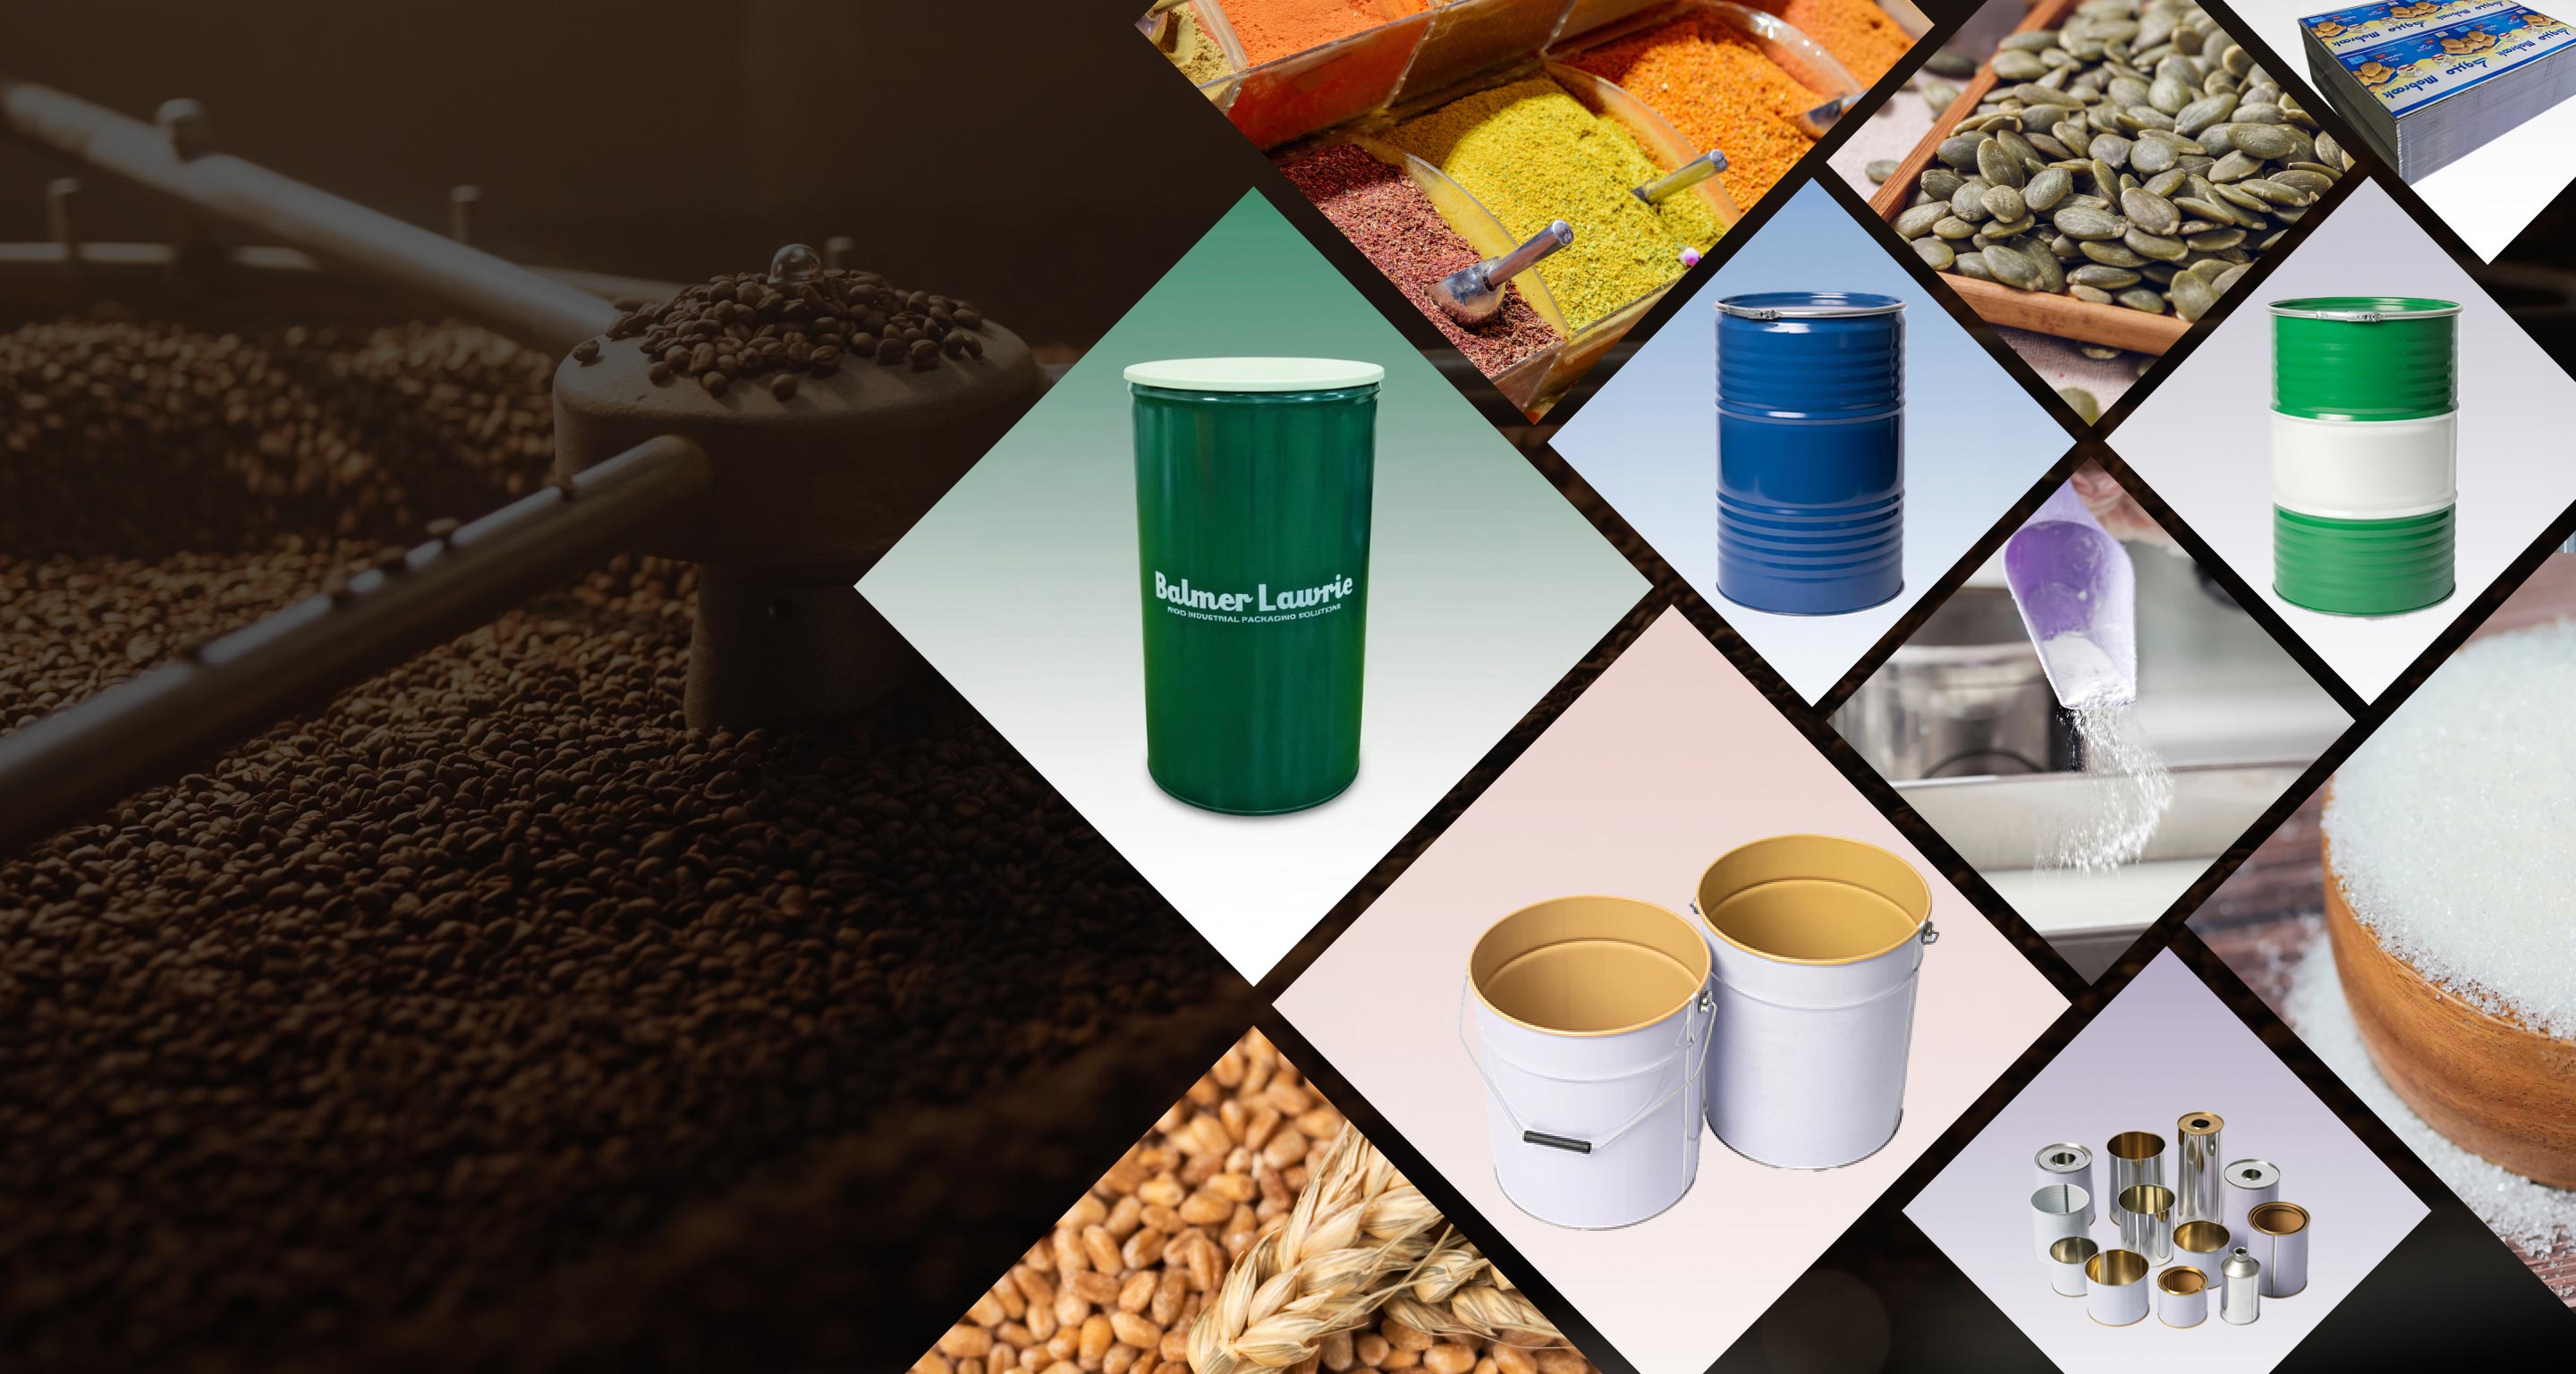
A comprehensive range of steel drums, tinplate containers, and PPCP packaging solutions designed for dry food applications.